Key Differences
1. Frequency Range & Heating Depth
- MF Induction:
- Frequency: 1–10 kHz
- Heating Depth: Deep penetration (2–10 mm).
- Effect: Uniform through-thickness heating, ideal for thick-walled pipes (≥10 mm).
- HF Induction:
- Frequency: 10–50 kHz
- Heating Depth: Shallow penetration (0.5–2 mm).
- Effect : Rapid surface heating, suited for thin-walled pipes (≤10 mm).
2. Temperature Control & Uniformity
- MF:
- Lower thermal gradient ( ΔT ≈ 30–50°C between inner/outer walls).
- Reduces risk of cracks/oxidation in critical alloys (e.g., stainless steel).
- HF:
- High thermal gradient (ΔT ≈ 100–200°C).
- Risk of overheating/burning thin walls.
3. Efficiency & Quality
- MF:
- Slower bend rate (0.5–1.5°/s) but superior dimensional accuracy (meets ASME B16.49 ovality ≤3%).
- Minimal spring back, better surface finish.
- HF:
- Faster bend rate (1.5–3°/s), but higher risk of deformation/ovality.
- Cost-effective for simple bends.
4. Industry Preference
- MF Dominates: 90%+ of heavy industrial bending (power plants, pipelines) due to reliability and compliance with strict standards (ASME/API).
- HF Niche: Repairs, thin-wall tubing, or budget-limited scenarios.
—
How to Choose between MF and HF
- Use MF If:
- Pipe wall thickness >10 mm or diameter >DN 200.
- Material is stainless steel, duplex, or high-alloy.
- Precision bending (e.g., nuclear/offshore applications) is required.
- Use HF If:
- Thin walls (<10 mm), small pipes (<DN 200).
- Rapid, low-cost bending for non-critical systems.
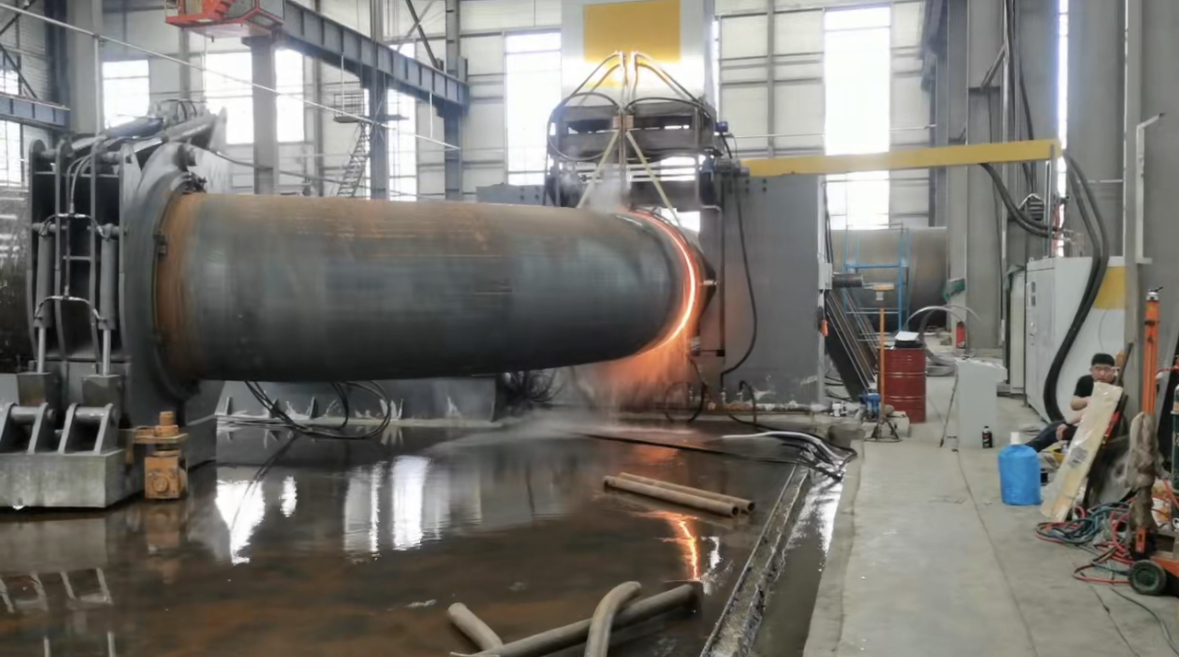
> Modern Trend: Advanced MF systems (with IGBT inverters, 1–20 kHz adaptive frequency) now dominate both thick and thin-wall bending, replacing HF in most industrial applications.
Post time: Jul-07-2025


